-

+86-13404286222
-

hmjxboss@gmail.com

INQUIRE NOW
+86-13404286222
hmjxboss@gmail.com
INQUIRE NOW
These parts behave differently from ordinary machined components, because a rotor is one piece that has to satisfy mechanical, thermal and aerodynamic requirements at the same time. Every requirement is written into the drawing long before the first cut is taken, which is why five decisions outweigh any supplier discount: duty envelope, material grade, starting stock, inspection scope and supplier route.
A rotor enquiry becomes comparable only once five numbers are fixed on paper: rated speed, trip speed, bearing span, gas composition and discharge temperature. Without them, every supplier prices a different machine and the quotations cannot be compared line by line.
The reason is mechanical rather than commercial. Critical speed, journal diameter, seal clearance and balance grade all follow from those inputs. A supplier quoting a 9,000 rpm rotor for dry gas will size journals and impeller fits differently from one quoting a 3,000 rpm machine for wet, corrosive service, even when both drawings show the same overall length.
The stator side matters as much as the rotor. Bore diameter, diaphragm fits and nozzle geometry belong to the compressor cylinder, so buyers building a complete stage usually place the shaft and the housing on one purchase order and keep the mating dimensions inside a single quality system.
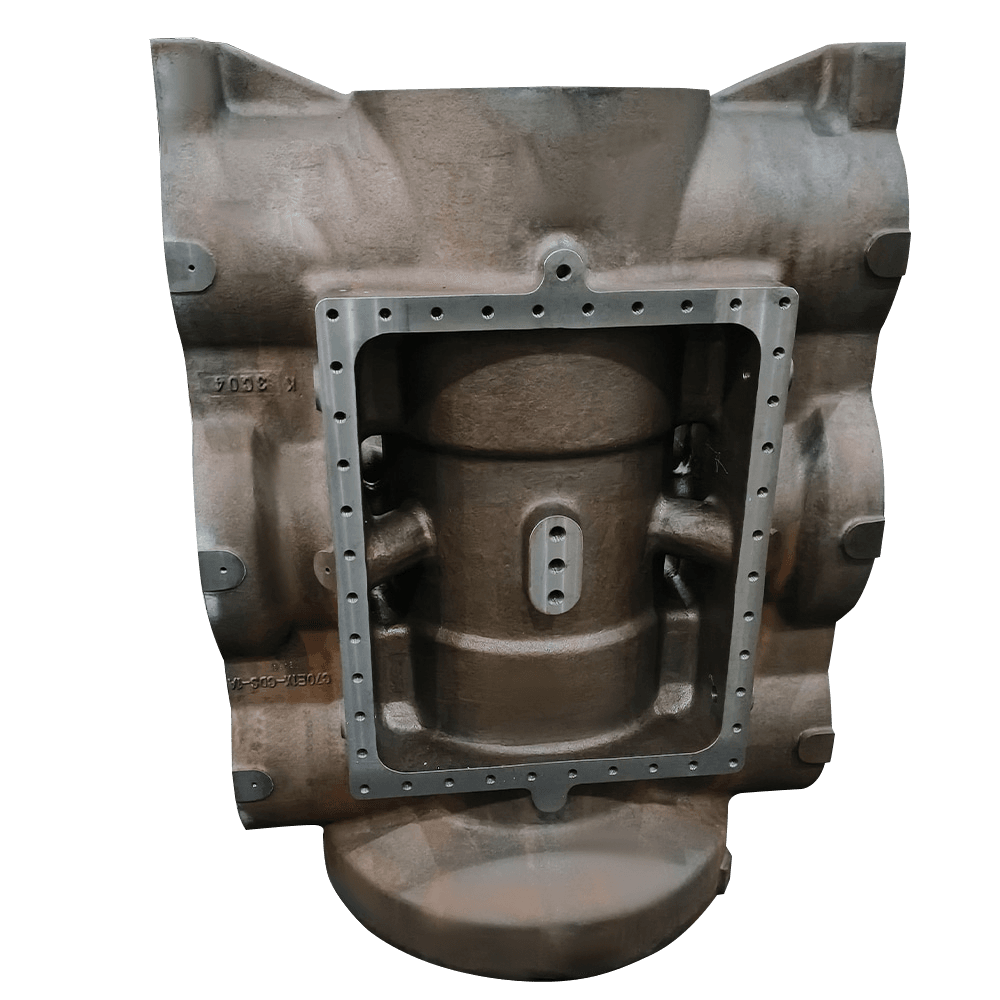 Casting of Compressor Housing ManufacturersLarge compressors usually adopt heavy-duty structural designs, which can withstand high-intensity loads and therefore have strong continuous operation capabilities. Ad...View Product →
Material grade is the largest single cost driver on a rotor order, and the item most often chosen by habit instead of by service condition. A rotor in 34CrNiMo6 forged stock costs a fraction of an equivalent part in Inconel 718, and the gap comes from three places: ingot price, forgeability, and the heat treatment and testing hours the grade demands.
| Material | Typical service | Sourcing implication |
| 42CrMo4 (1.7225) forged | Air and inert gas, moderate temperature | Lowest cost per kg, widest availability in large open-die forgings |
| 34CrNiMo6 (1.6582) forged | Process gas rotors with torque and shock loading | Standard choice for large shafts, needs a controlled heat treatment cycle |
| Duplex stainless 2205 | Chloride-bearing, seawater-cooled or wet service | Narrow forging window, ferrite content and UT checks add time |
| 17-4PH (1.4542) | Corrosive service at moderate temperature | Strong and machinable, but not a high-temperature solution |
| Inconel 718 (UNS N07718) | High temperature and sour gas at high stress | Longest lead time and highest cost, with minimum order sizes |
Sour-service rotors usually need more than one grade. Sleeves, bushings and seal components in Inconel 718 (UNS N07718 / 2.4668) are frequently specified alongside the main alloy steel forging, and a supplier already holding Inconel 718 forged parts, pipes, sleeves and bushings removes a second purchasing channel from the schedule.
Forged stock is the default for large compressor shafts and rotors, and it stays the right answer whenever the part carries bending load, high torque or a high-speed balance requirement. Casting wins only where the geometry is a body with internal passages or irregular walls, which is why castings dominate housings and cylinder bodies while forgings dominate rotors.
Buying the rotor and a forged body from one supplier shortens the sequence: one heat treatment philosophy, one ultrasonic acceptance class, one set of dimensional records.
 Forging Casting Parts Processing ManufacturersForging and casting are both important metal processing methods in the industry, and they have wide-ranging applications. They have significant differences in terms of...View Product →
A rotor drawing without an inspection plan is an invitation to argue at final acceptance. Name the checks, the acceptance limits and the reporting format in the purchase order, because a supplier that reports only final dimensions leaves the buyer with no evidence about what is inside the forging.
| Check | Method | What it protects |
| Internal soundness | Ultrasonic examination of the forging to an agreed acceptance class | Keeps porosity and forging laps away from high-stress journals |
| Surface integrity | Magnetic particle inspection on journals, keyways and fillets | Catches cracks and seams in the zones that fail first |
| Grade and heat treatment | Ladle analysis with tensile and impact tests on a test coupon | Confirms the material and cycle actually delivered |
| Journal geometry | Micrometer and runout measurement over the full bearing length | Protects bearing fit, oil film and vibration behaviour |
| Surface finish | Roughness measurement on journals and seal seats | Prevents seal wear, with 0.4 to 0.8 Ra a common callout |
| Dynamic balance | Two-plane balancing to an agreed grade | G2.5 or finer, which high-speed service normally requires |
Twelve to twenty weeks from purchase order to shipment is normal for a forged, fully machined alloy steel rotor. Anything promised inside eight weeks is credible only if the forging already exists in inventory, and the schedule below shows where that time actually goes.
Documentation separates capable suppliers from assemblers. A rotor package should arrive with material certificates traceable to the heat number, heat treatment charts, NDT reports with operator certification, dimensional and runout records, a balance report and the machining route card.
Jiangyin Huanming Machinery Co., Ltd. machines large parts on horizontal and gantry machining centres, CNC boring mills and high-speed vertical lathes, and runs magnetic particle, ultrasonic, hardness and roughness testing in house. For rotors that matters, because inspection can be repeated at each operation instead of only at the end.
In a geared compressor train the rotor is only half of the dynamic system, so many buyers order the speed-increasing drive components together with the shaft and keep one alignment and balance philosophy across the whole train.
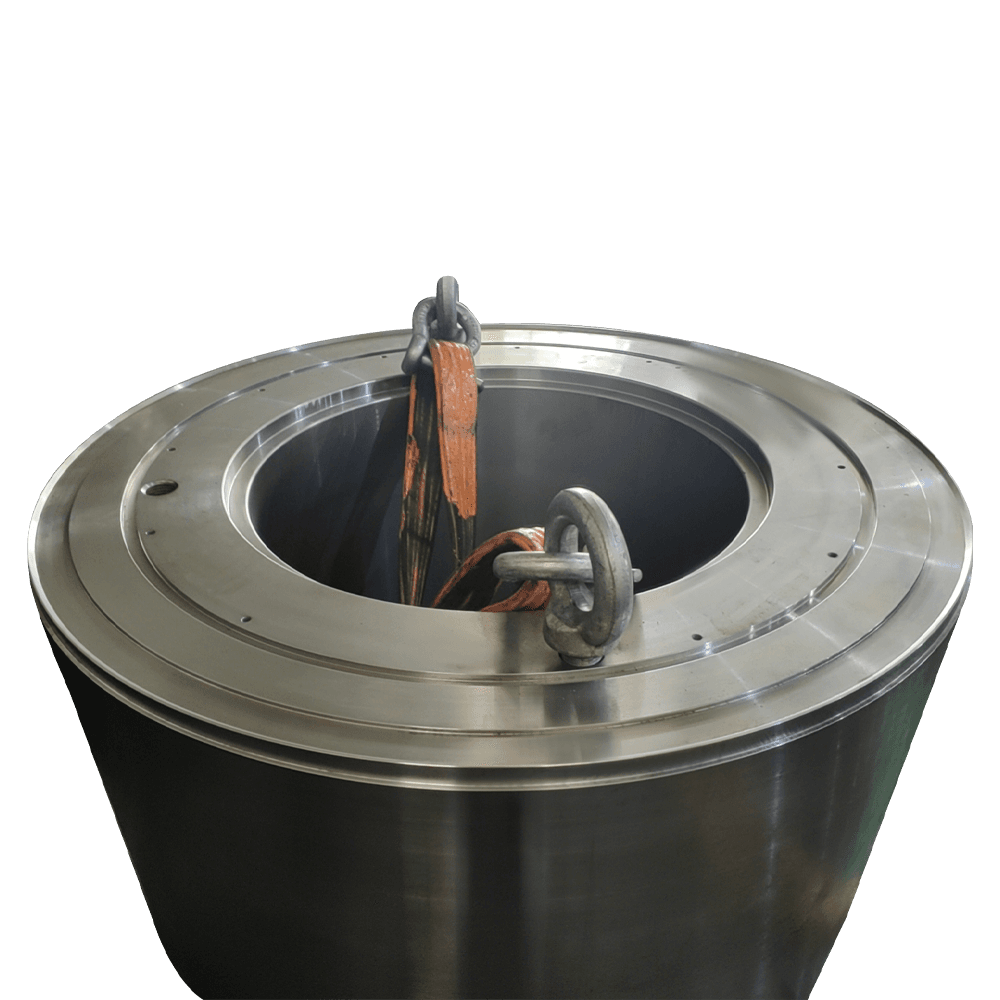 High Speed Transmission Pinion ManufacturersHigh-speed transmission gears are key components used in high-speed rotating mechanical systems. They are designed and manufactured to achieve efficient and smooth pow...View Product →
For the engineering view of the same trade-offs, this note on material selection for a large compressor shaft rotor follows the grade decisions from the design side.
Work the sequence in order. Most scrapped rotors trace back to a step that was skipped between the enquiry and the purchase order.
34CrNiMo6 forged steel covers most process gas rotors in air and inert service. Move to duplex 2205 when chlorides are present, and to Inconel 718 only when temperature, sour gas or stress genuinely demand it, because the cost and lead time penalty is substantial.
Plan on 12 to 20 weeks for a forged rotor between 1 and 8 tonnes, including heat treatment, machining, balancing and documentation. Special alloys add four to eight weeks, and ordering the forging early recovers part of that.
Material certificates traceable to the heat number, heat treatment charts, ultrasonic and magnetic particle reports, dimensional and runout records, a two-plane balance report and the machining route card. Reject any package that cannot show all six.
Yes, and it is usually the better route. Bore diameter, diaphragm fits and seal clearances couple the stator to the rotor, so one supplier holding both parts keeps the mating dimensions under a single quality system and removes arguments about which side caused the clearance problem.
 No. 16 Dayuanli Road, Yunting Street, Jiangyin City, Jiangsu Province, China
 +86-13404286222 / +86-13404286222
 +86-510-86668678
 hmjxboss@gmail.com
Copyright © Jiangyin Huanming Machinery Co., Ltd. All Rights Reserved.Custom Large Components Mechanical Processing Manufacturers
 English
 中文简体
 русский
 日本語
 Español
